Home > News > Industry News
Introduction
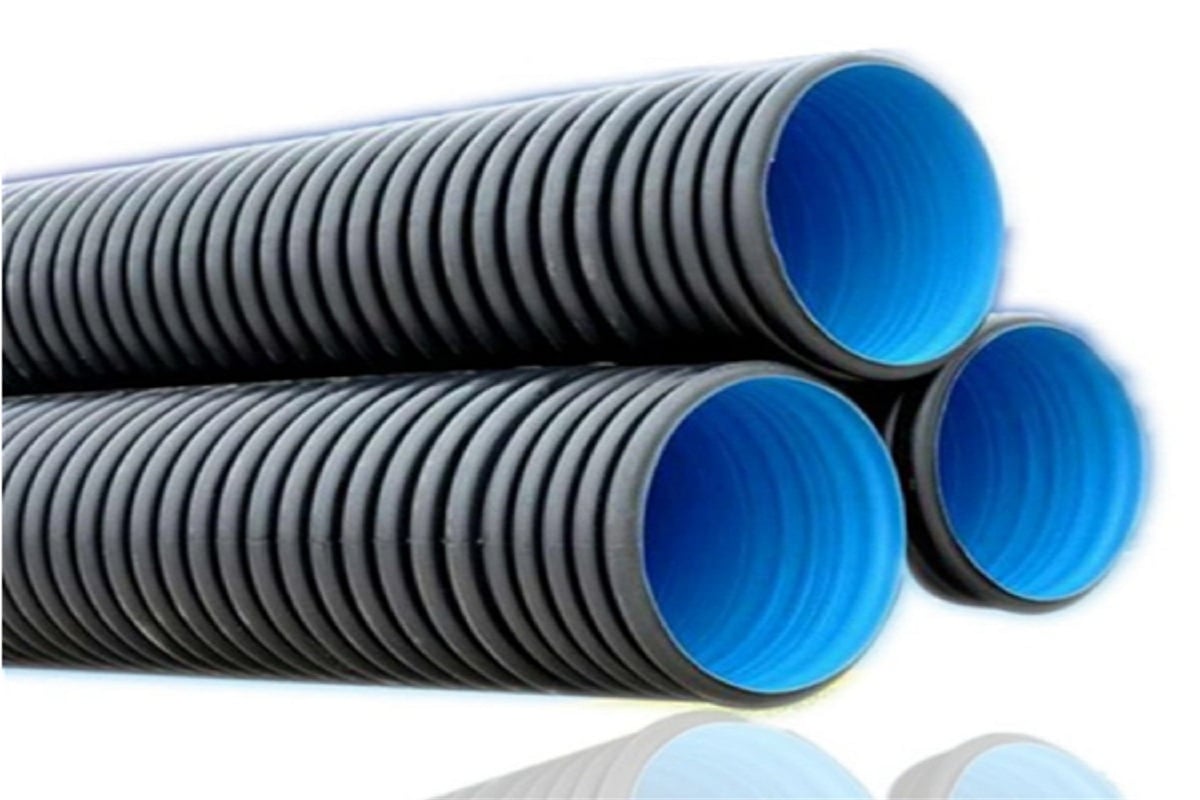
HDPE Double Wall Corrugated Pipe (DWC Pipe) is a mainstream lightweight structured drainage pipe widely used in global municipal and civil engineering. Adopting one-time extrusion molding and vacuum sizing technology, it features a unique dual-layer structure: a smooth inner wall for efficient water flow and a hollow annular corrugated outer wall for high compression resistance. With balanced performance, affordable cost, and convenient installation, it has become the most popular solution for conventional rainwater sewage drainage, seepage drainage, and cable protection projects.
Core Performance Features
The dual-wall hollow structure is the biggest highlight of HDPE double wall corrugated pipe. The smooth inner wall has an extremely low friction coefficient, effectively reducing water flow resistance, accelerating rainwater and sewage discharge, and avoiding pipeline blockage, which ensures efficient and stable drainage capacity for a long time. The annular corrugated outer wall enhances the pipe’s overall toughness and ring stiffness, enabling it to bear external soil pressure and ground load, adapting to various buried ground conditions and resisting slight foundation settlement.
In terms of durability, the high-quality HDPE material provides excellent anti-aging, anti-ultraviolet, and corrosion resistance. It is immune to acid-base substances in soil, domestic sewage, and general industrial wastewater, with no rust, scaling, or degradation. The pipe can serve stably for more than 50 years in conventional buried environments, far superior to traditional cement pipes and ordinary plastic pipes.
Superior Construction & Economic Benefits
HDPE double wall corrugated pipe is lightweight, flexible, and easy to transport and stack, which greatly saves transportation costs and on-site storage space. The pipe adopts flexible rubber ring socket connection, with simple operation and fast installation speed, no professional welding equipment required. This connection method ensures good sealing performance, effectively preventing pipeline leakage, and greatly improves construction efficiency compared with traditional pipe laying processes.
In addition, the product has complete specifications, covering multiple ring stiffness grades including SN4, SN8, SN12.5 and SN16, and a full range of diameters from DN100 to DN1000. It can flexibly match different project load and drainage demands, with high project adaptability and overall cost advantages, helping customers optimize engineering budgets and improve project efficiency.
Diversified Application Fields
HDPE double wall corrugated pipe covers almost all conventional drainage and protection scenarios: municipal urban rainwater and sewage diversion systems, residential community drainage pipelines, highway and railway underground seepage and drainage projects, airport and square ground drainage, farmland irrigation and drainage, industrial park domestic sewage discharge, and power communication cable protection casing. It is a versatile and cost-effective pipeline product for civil and municipal infrastructure construction.
Conclusion
With its efficient drainage performance, reliable structural strength, excellent durability, and outstanding cost performance, HDPE double wall corrugated pipe has become a benchmark product in the field of medium and light-duty drainage pipelines. It provides stable, economical, and environmentally friendly pipeline solutions for global municipal construction, civil engineering, and agricultural water conservancy projects, and is widely recognized and adopted by engineering teams worldwide.

Shijiazhuang Shentong provides high-quality HDPE, PPR, and PEX pipes for building, municipal, and industrial applications. OEM/ODM services, ISO-certified production, and export to 60+ countries. Request free samples today.
Luancheng District, Shijiazhuang City, Hebei Province.
Copyright © 2025 by Shijiazhuang Shentong Plastic Industry Co., Ltd. Privacy Policy
 EN

 Hot News